Colour and Variant Verification: How the Process Works
Follow a colour inspection trial from approved reference samples to lighting, part tracking and challenge results. Define acceptable variation before choosing cameras.
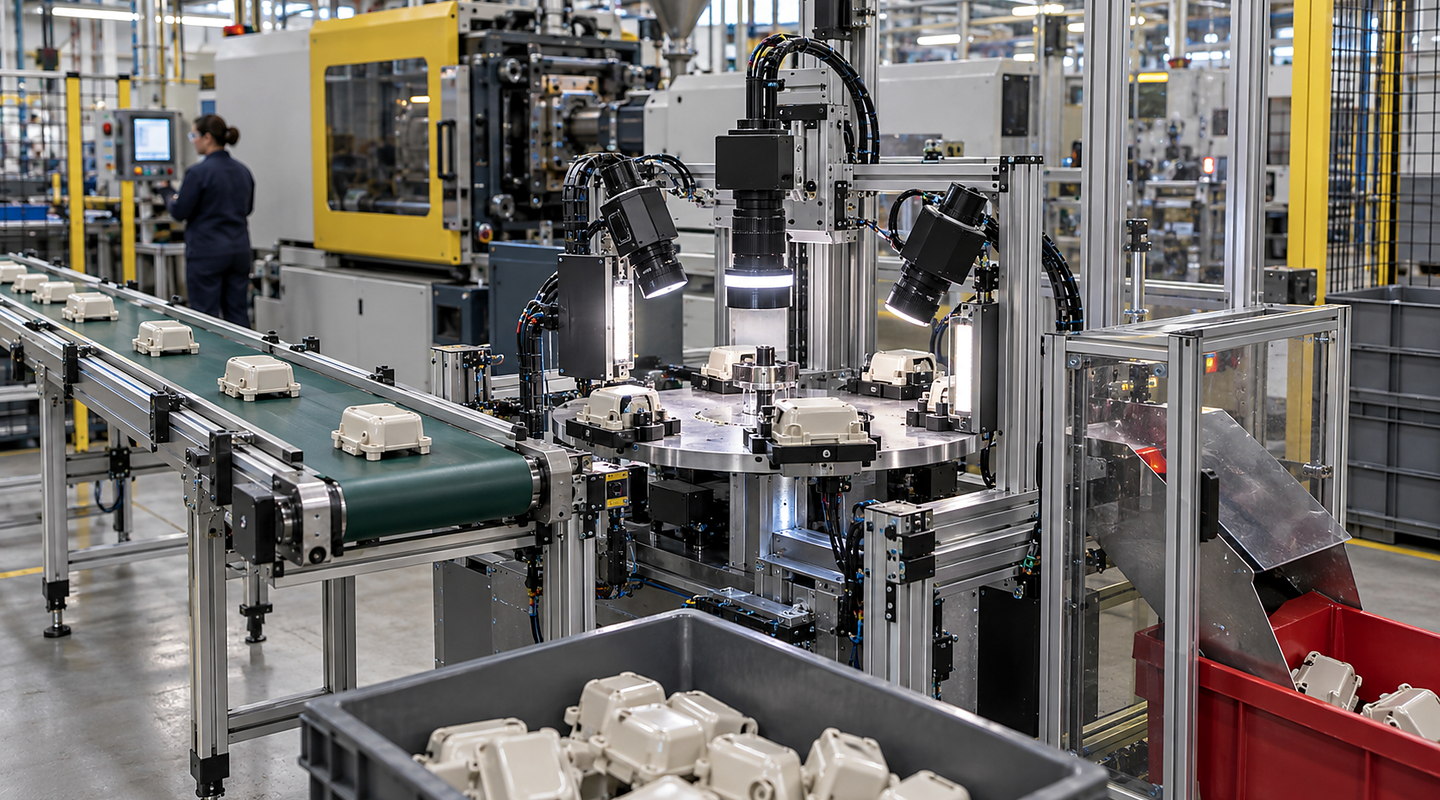
Photographs illustrate general machine-vision inspection. Colour and variant decisions must be assessed using representative products, agreed reference samples and the intended lighting and presentation.
Start with the colour or variant decision the line must make and approved acceptable, unacceptable and marginal examples. Trial those samples under the intended lighting, background, presentation and speed. Keep each result with the correct part and recipe, then record false accepts, false rejects and the agreed response to uncertain or missing results.
Use the colour inspection comparison checklist and agree the challenge-test record. The trial must distinguish acceptable production variation from the condition that needs rejection.
Understand the complete route from input to accepted output — Colour and Variant Verification
Plan colour and variant verification around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. Follow the material or part through each operating step and include recovery, cleaning and change in the real cycle.
Discuss your application

Four clear stages for colour and variant verification
At each stage, you can review how visible defect or measurement definition for colour & variant verification and false-accept, false-reject and challenge criteria affect the next commitment.
- 01
Define the Visible Decision and Collect Representative Samples
Define the required colour or variant decision and its acceptance boundary. Identify approved good, bad and marginal samples, including normal finish, batch, supplier and product variation, and name who may approve references and recipe changes.
- 02
Prove Contrast, Presentation and Timing in an Optical Trial
Compare the approved samples using the intended lighting, background, product position and production-speed range. Check that acceptable variation remains distinguishable from the colour or variant condition that must be rejected.
- 03
Integrate Cameras, Controls, Reject Handling and Recipes
Associate the inspection result with the correct part and active recipe through the agreed reject or line-control response. Include incorrect, uncertain and missing results, recipe changes, fault indication and controlled recovery.
- 04
Challenge Marginal Cases and Document Agreed Results
Use the agreed method, repetitions, acceptance limits and result record to challenge good, bad and marginal cases. Record false accepts and false rejects under the intended conditions, plus unresolved cases and how later changes are controlled.
Decisions and results stay connected
| Stage | What happens | What you can review |
|---|---|---|
| Define the Visible Decision and Collect Representative Samples | Define the required colour or variant decision and its acceptance boundary. Identify approved good, bad and marginal samples, including normal finish, batch, supplier and product variation, and name who may approve references and recipe changes. | Identified reference samples, approved classifications, acceptance boundaries, normal variation and change-approval responsibility. |
| Prove Contrast, Presentation and Timing in an Optical Trial | Compare the approved samples using the intended lighting, background, product position and production-speed range. Check that acceptable variation remains distinguishable from the colour or variant condition that must be rejected. | Sample identity, lighting, background, finish, presentation, timing and the observed colour or variant decision. |
| Integrate Cameras, Controls, Reject Handling and Recipes | Associate the inspection result with the correct part and active recipe through the agreed reject or line-control response. Include incorrect, uncertain and missing results, recipe changes, fault indication and controlled recovery. | Correct part-to-result and recipe association, reject or line response, fault indication and observed recovery. |
| Challenge Marginal Cases and Document Agreed Results | Use the agreed method, repetitions, acceptance limits and result record to challenge good, bad and marginal cases. Record false accepts and false rejects under the intended conditions, plus unresolved cases and how later changes are controlled. | Expected and observed decisions, separate false-accept and false-reject records, unresolved cases and change controls. |
Keep connected responsibilities clear
Your final colour and variant verification scope must also account for recipe, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.
- A camera can only assess a property made visible and repeatable by the inspection setup.
- Sample diversity and marginal cases determine how meaningful a feasibility result is.
- Visual inspection does not replace hidden, destructive, functional or statutory tests.